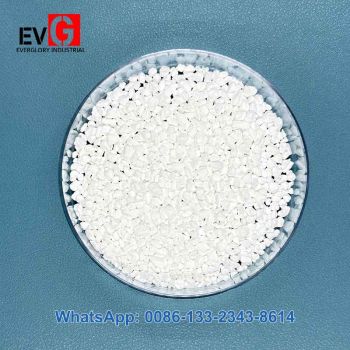
High-Purity Calcium Hypochlorite 70% Granular – Industrial & Municipal Water Disinfection Solution
As a trusted global supplier of water treatment chemicals, we deliver premium-grade Calcium Hypochlorite 70% in granular form, specifically manufactured to meet the rigorous demands of industrial, municipal, and commercial applications. Engineered for optimal stability, high chlorine availability, and fast dissolution, our product provides an economical and powerful solution for large-scale shock treatment, continuous sanitization, and pathogen elimination.
Technical Specifications & Product Advantages
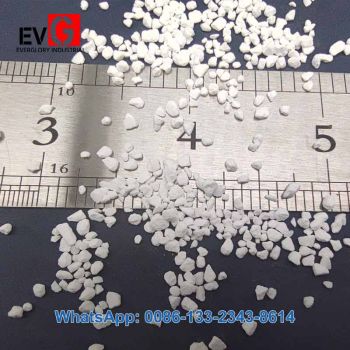
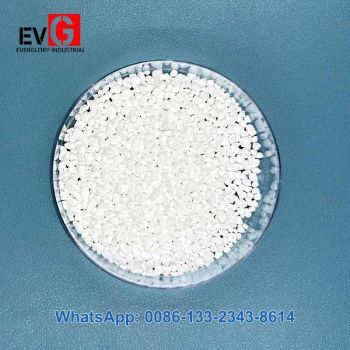
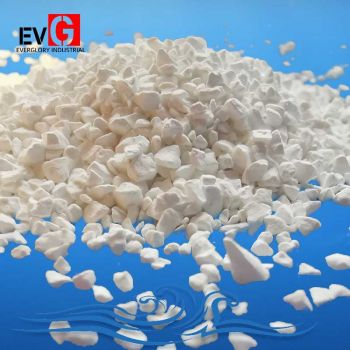
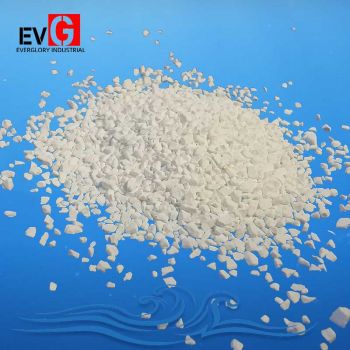
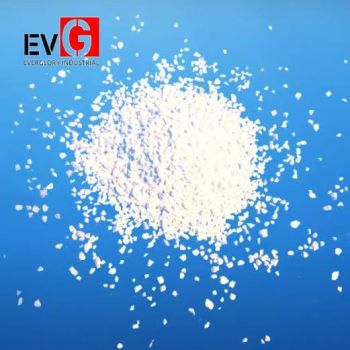
Our Calcium Hypochlorite 70% features a advanced granular formulation produced via the sodium process, ensuring low insoluble matter and superior storage stability.
| Specification Parameter |
Value / Standard |
| Active Chlorine Content |
70% min. |
| Physical Appearance |
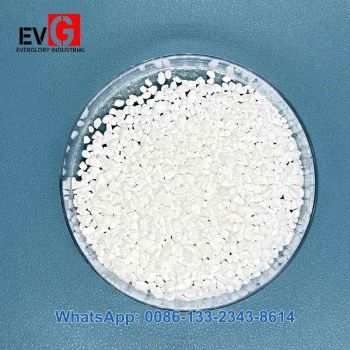
White or Off-White Granular |
| Moisture Content |
(Hydrated Grade) |
| Annual Supply Capacity |
50,000+ Metric Tons |
| Standard Packaging |
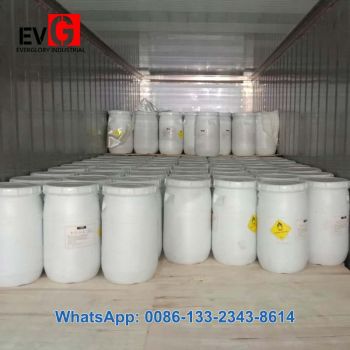
45kg / 50kg UN-Approved HDPE Drums with Inner Liner |
Key Benefits for B2B Buyers
• High Chemical Efficiency: Delivering 70% available chlorine, our granular product reduces shipping costs per unit of active disinfectant compared to lower-concentration alternatives.
• Rapid & Clean Dissolution: The uniform granular mesh size prevents caking, minimizes dust hazards during dosing, and dissolves quickly without leaving excessive sludge.
• Extended Shelf Life: Advanced hydration technology minimizes chemical degradation during ocean transit and long-term warehousing in warm climates.
• Global Compliance: Fully compliant with ISO, SGS, and international water treatment certification standards for safe handling and import clearance.
Primary Applications & Industry Solutions
Our high-potency Calcium Hypochlorite 70% in granular form is widely deployed across critical industries requiring reliable antimicrobial control:
1. Swimming Pool & Water Park Sanitation: Excellent for rapid shock dosing (superchlorination) to kill algae, destroy chloramines, and maintain crystal-clear water quality in commercial pools.
2. Municipal Drinking Water Treatment: Efficiently neutralizes waterborne bacteria, viruses, and pathogens in water purification plants and rural supply networks.
3. Industrial Effluent & Cooling Towers: Controls bio-fouling, slime buildup, and Legionella risks in recirculating cooling systems and industrial wastewater facilities.
4. Agricultural & Food Processing: Ideal for equipment sanitization, livestock housing disinfection, and fruit/vegetable washing solutions.
Supply Chain & Global OEM/ODM Services
We support international importers, distributors, and municipal contractors with flexible, end-to-end B2B solutions:
• Customized Packaging: Standard UN-certified drums (plastic/iron), customizable private label branding, and multi-language safety handling labels.
• Strict Quality Assurance: Batch-to-batch testing via internal QA and third-party inspections (SGS/BV) prior to shipment.
• Dangerous Goods (DG) Logistics Expertise: Full support with IMO/Class 5.1 hazardous goods documentation, MSDS, and optimized container loading to lower logistics overhead.
Partner with us for dependable quality and direct factory pricing.
Contact our chemical engineering team today to request a formal quotation, COA (Certificate of Analysis), or free sample batch.